OEM RFID antenna manufacturing moves from a prototype that answers a design question to a released assembly that another team can build and inspect. That transition requires controlled drawings, material definitions, test methods, and a clear decision about which prototype changes are accepted for production.
Define what the OEM supplies and approves
The buyer should identify the requirement owner, design authority, drawings, bill of materials, reader interface, mechanical envelope, and acceptance criteria. Clarify who supplies the reader, cable, tags, fixture, and host enclosure used for validation. If design work is shared, define which party approves RF tuning and mechanical changes.
The term OEM does not settle ownership of tooling, design files, or test data. Put those responsibilities in the agreed deliverables before prototype work becomes dependent on them.
Use each build to answer a different question
| Stage | Main purpose | Evidence needed before proceeding |
|---|---|---|
| Engineering prototype | Examine feasibility and tuning variables | Identified sample, drawing, deviations, feed and relevant RF results |
| Integrated prototype | Check the reader, antenna, enclosure, and tags together | Installed configuration, test method, observations, and corrective actions |
| Production-intent build | Check the intended materials, interfaces, and assembly method | Current drawing and BOM, inspection results, and correlation with the accepted design |
| Production release | Enable repeatable build and acceptance | Released files, limits, fixtures, work instructions, traceability, and change rules |
An early prototype may use a temporary cable or accessible tuning arrangement. Mark those differences explicitly. Measurements from that build should not be carried into a final report as though the production assembly were identical.
Turn prototype learning into manufacturing controls
Record which dimensions, materials, feed features, solder joints, adhesives, or cable positions affect RF behavior. Give each critical feature an inspection or verification method. If a tuning component remains in the design, define its approved value or adjustment range and the check required after adjustment.
Use representative builds to examine variation, then agree how first-article, sampled, and routine production checks relate to the engineering validation. Record the lot size, inspected characteristics, results, and disposition of exceptions.
Prepare a usable release package
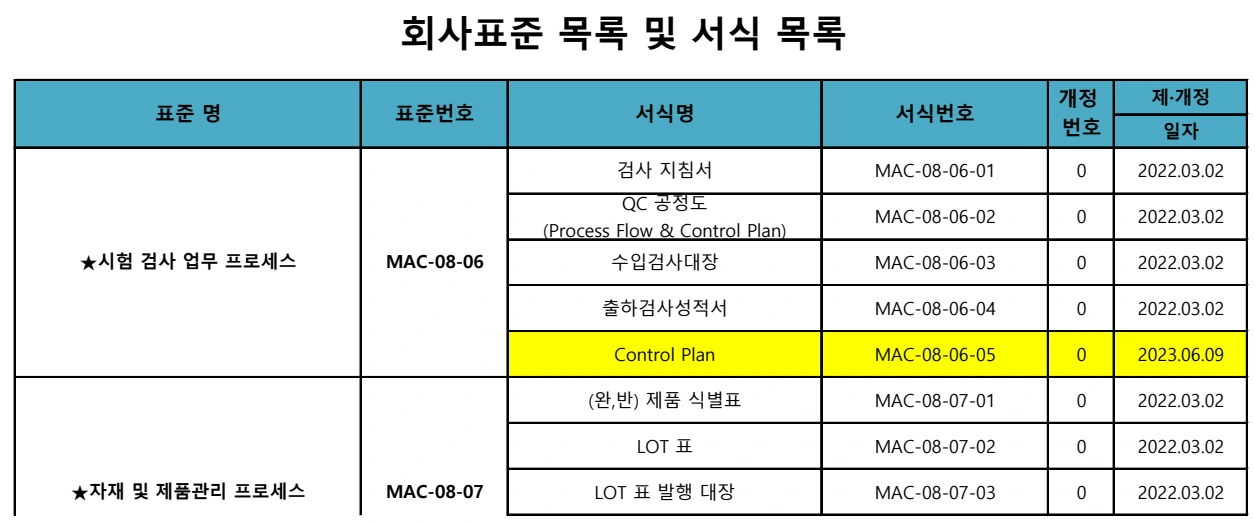
The manufacturing team needs the drawing and BOM revision, approved substitutions, assembly instructions, fixture definition, instrument settings, acceptance limits, and result-record format. Include the handling of rejected parts and the authority to approve rework or deviations.
For reader antennas, production RF checks should use a stated reference plane. Application acceptance should preserve the reader configuration, tags, mounting, and enclosure used to demonstrate the intended read zone. A rapid production check may detect assembly drift without repeating every characterization test; its purpose and correlation need to be defined.
Control changes after release
Material, connector, cable, housing, process, or drawing changes can affect the accepted RF state. State which changes require notification, approval, and retesting. Keep the reason for each critical tolerance in the design record so a later cost reduction does not remove an important control.
For an OEM discussion with MAC technologies Inc., provide the requirement, drawing and BOM, prototype history, expected production scope, acceptance method, and deliverables. Identify who will approve the design, process and test records before release.
References
GS1 EPC UHF Gen2 Air Interface Protocol
IEEE 149-2021 Recommended Practice for Antenna Measurements
https://www.gs1.org/standards/rfid/uhf-air-interface-protocol
https://standards.ieee.org/ieee/149/6667/